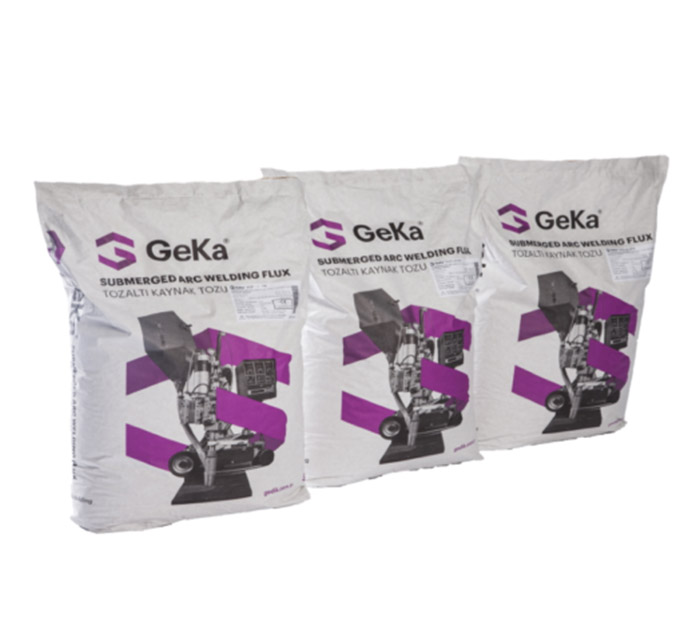
Флюс сварочный ELIFLUX PIPE

Категория:

Описание

Standards
TS EN ISO 14174 SA AB 1 78 AC H5
EN ISO 14174 SA AB 1 78AC H5
AWS A5.17 F7A4-EM12
AWS A5.23 F7A4-EA2-A2 / F8A4-EA4-A4
Chemical Composition of Weld Metal % (Typical)
SAW — Wire C Si Mn Mo
S2 0.05 0.40 1.35 —
S2 Mo 0.06 0.40 1.40 0.50
S3 Mo 0.06 0.40 1.60 0.45
Mechanical Properties
SAW Wire AWS A5.17 / AWS A5.23 Yield Strength (N/mm²) Tensile Strength (N/mm²) Elongation ((Lo=5do) (%)) Impact Strength (ISO-V/ 0°C) Impact Strength (ISO-V/-20°C) (Joule) Impact Strength (ISO-V/-40°C)
S2 F7A4-EM12 460 550 26 — 75 J 50 J
S2 Mo F7A4-EA2-A2 510 640 25 — — 60 J
S3 Mo F8A4-EA4-A4 530 620 25 100 J — 50 J
Features and Applications
  • SAW flux type composed of agglomerated aluminate Basic.
  • Basicity of the flux According to Boniszewski Formula is 1.7
  • Excellent removal of slags of weld beads formed at high temperatures
  • Suitability for use in both bilateral and tandem (AC/DC) welding operations.
  • Sufficiently high tougness of weld metals obtained particularly by 2-pass welding operations.
  • Suitability for use in welding of high-strength steels.
  • Process requirement of re-drying at 300°C — 350°C for 2 hours.
Basicity
Basicity 1.7
Operating Data
Product Code Package Weight (Kg) Package Type
3010800019 25 Kraft Bag
3010800057 Kraft Torba 25

Оставить заявку

Нажимая на кнопку «Отправить заявку», вы соглашаетесь на обработку персональных данных и политику конфиденциальности